MAPAL is strengthening its machining solutions for constant velocity (CV) joints through developments in cutting material grades and tool design, aiming to improve production efficiency in 2026.
Polycrystalline cubic boron nitride (PcBN) remains a key cutting material for machining hardened steel, particularly in demanding applications such as CV joint manufacturing. Drawing on its longstanding association with CV joint manufacturers, MAPAL is applying its expertise to optimise machining processes for these components.
The latest developments focus on the targeted improvement of cutting material grades and tool design to enhance machining efficiency and meet the requirements of CV joint production.
High demands in the hard machining of CV joints
Depending on the vehicle type, various designs of drive joints are used in automotive engineering, both on the wheel side and on the transmission side. The main components include the outer housing, also known as the outer race, the ball hub (inner race) and the ball cage. The balls run in specially shaped tracks between the inner and outer race and are guided by the cage in such a way that constant rotary motion is possible even at an articulation angle, for example in the case of a steering movement.
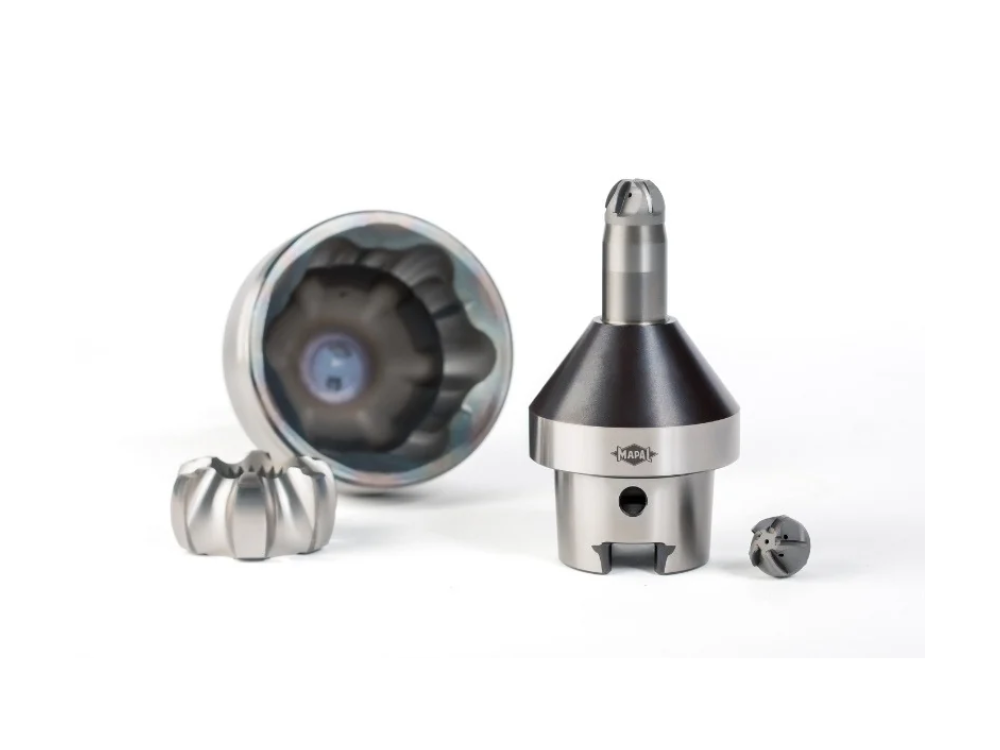
The ball tracks on both the inner race and the outer race have to be hard milled. The requirements for form and surface are very high at this point, which is why the geometric design of the milling cutter plays a decisive role. MAPAL precisely matches its ball track milling cutters to the tolerances required on the component. In addition to the geometry of the tool, the cutting material used and the cutting-edge preparation are important for tool life, performance and the surface quality achieved.
Cutting material development specifically aligned with process requirements
With its experience, MAPAL is able to develop cutting materials specifically for machining certain components. The new uncoated PcBN cutting material FU240 is tailored to the requirements of hard milling the ball tracks on the outer race, while cutting material FU290 is correspondingly tailored to those of the inner race. Different PcBN substrates are generally applied to take account of the different machining characteristics of the inner and outer race and the associated wear mechanisms on the tool. The industry also uses different materials for the two components: Tempered steels for the outer race, and usually case-hardened steels for the inner race. While automotive manufacturers each follow their own philosophy in terms of shaping and especially ball guidance, the materials are largely standardised.
Significantly higher tool life quantity in milling
In order to successfully improve its PcBN cutting materials and thereby secure its technological lead, MAPAL – as a technology partner – draws on a deep understanding of the entire process. To achieve longer tool lives when machining CV joints, the task was to find the optimum balance between high abrasion and diffusion resistance with sufficient ductility. Development parameters included the CBN content of the cutting material, grain sizes and the composition of the binder. The initial results demonstrate a significant increase in the tool life achieved by the new cutting materials: compared with the materials previously used, the new grades FU240 and FU290 improved the tool life by more than 30 percent at cutting speeds in the range of 180 m/min and a feed per tooth of between 0.07 and 0.10 mm.
Five-edged milling cutter design reduces machining time and unit costs
This does not yet take into account the influence of a new five-edged tool design for the ball track milling cutters, which MAPAL is also presenting for the first time in 2026. Until now, four-edged designs have been the state of the art in practice. The additional cutting edge reduces machining time by around 20 percent compared with the four-edged milling cutter. The engagement time per cutting edge for each ball track is shorter, which has an additional positive effect on tool life. With annual production volumes of around 15 million components, these two effects together produce considerable savings potential in terms of unit costs.
New cutting materials also deliver significant gains in hard turning
New PcBN cutting materials from MAPAL are also being used for hard turning, with the initial focus here again on machining drive joints. Grade FP240 is intended for continuous-cut applications, such as on the shank of the outer race. For interrupted cuts, such as those occurring on the inner race and the cage, the more ductile grade FP260 is used. Both are PVD-coated and achieve tool lives that are a good 40 percent higher than those of conventional cutting materials.
The gradual introduction of the new ball track milling cutters and the PcBN turning inserts emphasise MAPAL’s ambition to continue to set new benchmarks for machining hardened components.